Let me start by saying this isn’t just some textbook blog post—dealing with residues on an explosives production line is the kind of hands-on, make-or-break stuff we’ve been working through for years as a production line supplier. If you’re in the industry, you know residues aren’t just a “cleanup thing”; they’re the stuff that causes line downtime, safety scares, and even product inconsistencies. Let’s cut through the jargon and get to the real, practical moves we’ve tested that actually work. Explosives Production Line
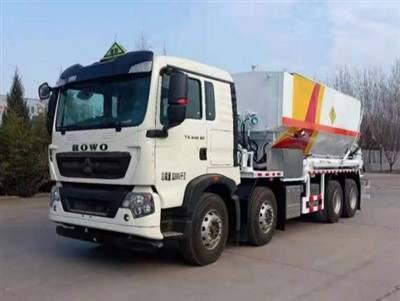
First off, let’s define what we’re actually talking about here. When we say residues on an explosives line, we’re not just talking about the leftover goop you see on equipment after a run (though that’s part of it). It’s unreacted explosive compounds, partially decomposed material, even trace amounts that get caked on conveyor belts, mixing tanks, and packaging parts. The worst part? That stuff is super unstable—leave it sitting, and even tiny sparks, static electricity, or excess heat can set it off. We’ve had clients come to us after their lines had a safety shutdown because they missed residue buildup on a mixer impeller, and that’s the exact kind of headache we’re here to prevent.
As a supplier, I see a lot of lines making the same mistake: they treat residue cleanup like an afterthought, not a core part of the production process. Most clients come to us focused on line speed or yield, but residues slow you down way more when they cause unplanned stops. So let’s break down the game plan, step by step, the way we train our clients to do it.
First, you’ve got to audit your line specifically to your products. Not all explosives residues are the same. If you’re making ANFO (ammonium nitrate fuel oil), your residue is usually light, dry, and easy to brush off—but it’s also highly hygroscopic, so it clumps up if there’s any humidity. If you’re making something like emulsion explosives, the residue is thick, oily, and sticks to every surface, plus it can decompose over time if not removed properly. We don’t do one-size-fits-all here—when we set up a line for a client, the first thing we ask is what they’re making, then we map every single surface that could hold residue, how much builds up per run, and under what conditions it’s most likely to shift. For example, one of our mining explosive clients was having residue issues on their conveyor transfer points, where dust would build up and fall back into the product, causing inconsistent blast results. We adjusted the transfer chutes to have sloped, self-cleaning surfaces and added a low-pressure air blast that activates between runs, and that cut their residue-related product defects by 80% in the first month. That’s not rocket science—it’s matching the solution to the actual problem on their line.
Next, set up a proactive, not reactive, cleanup schedule. I can’t stress this enough: waiting until the line is gunked up is a terrible idea. We recommend tiered cleaning, not just a big deep clean every shift. Let’s be real, you don’t have time to take the entire line apart every hour, so tier it: quick, in-situ cleans every production run, minor part cleans at the end of each shift, and a full deep clean only once a week (or less, depending on product). For the quick runs, we install automated spray nozzles that run a mild, residue-specific solvent right after the product is discharged—no need to take anything apart, it’s all controlled through the line’s HMI, so your operators don’t have to touch anything dangerous. For those who work with more sensitive materials, we also offer dry ice blasting attachments—no messy solvents, just CO2 pellets that blast residue off without scratching surfaces or leaving behind any foreign material (critical, because even tiny bits of extra material can mess up explosive composition). We had a client doing pellet explosives switch from manual scrubbing to our automated in-run spray system, and they reduced their manual labor for cleanup by 65%, plus they had zero incidents of operators coming into contact with residual explosive during cleans. That’s the win we sell, not just equipment—safety and efficiency.
Then there’s the storage and disposal of residues, which is another big part no one talks about. You can clean the line all you want, but if you’re tossing the residue in a flimsy bin next to the line, that’s a recipe for disaster. We design residue collection systems that are fully enclosed—they don’t let residual dust or fumes escape, and they’re made from static-dissipating materials, so there’s no chance of a spark from static build-up. Also, we integrate a small, in-line neutralization step for liquid residues (like emulsion leftovers) that stabilizes them right as they’re collected, so you don’t have to transport unstable material off-site. A lot of our older clients were handling residue by scooping it into 55-gallon drums on the line floor, and that’s how you get things like dust explosions when a drum is bumped. We’ve updated their lines with closed, vented residue bins that dump directly into a sealed holding tank, and the neutralization step means that when we pick up residue for disposal (yes, we handle that too for our clients), it’s already stabilized, so transport is way safer and cheaper.
Wait, let’s talk about operator training too—because even the best equipment is useless if your team doesn’t know how to use it right. I see so many lines get residue issues because operators skip the automated cleanup step to hit a production quota. We include on-site training for every client, not just a manual. We do hands-on sessions where we show them how residue builds up, what happens if they skip a clean, and even do a demo where we simulate a small residue-related issue so they know exactly what to look for. One of our clients had a team that was cutting corners on automated cleans, so we set up little sensors on the line that alert the supervisor if a clean is missed mid-run—they thought it was annoying at first, but after a couple of false alarms that would’ve turned into shutdowns, they love it now. We also have a regular check-in program where we come back every 6 months to tweak the residue process, because lines change—you might switch products, run at higher speeds, so your residue plan needs to change too.
Now, let’s address the tough stuff: what if you have old lines that can’t be retrofitted with new automated systems? We don’t just sell new lines—we work with existing facilities too. For example, if you’ve got a mixer that’s still working but has impeller blades that catch residue, we can install replaceable, static-dissipating liners instead of making you buy a whole new mixer. For conveyor belts that get residue caked on, we offer specialized belt scrapers that are adjusted automatically after each run, so they don’t wear out the belt but still get every bit of residue. We had a client with a 10-year-old production line that was having constant residue-related shutdowns, and we retrofitted just the residue collection and automated clean parts for 30% less than a new line, and they’ve had zero shutdowns from residue in 18 months. That’s the value we bring as a supplier—we don’t force you to replace everything, we fix the specific residue pain points you have.
Also, let’s get real about common mistakes we see clients make. First, using the wrong cleaning agent. If you use a solvent that’s too harsh, it can react with residual explosive and make it more unstable. If it’s too mild, it doesn’t do anything. We test all our suggested cleaners against the residues from the products we’re handling, so we know exactly what works without causing a reaction. Second, not accounting for static electricity. Residue is often fine dust, which builds up a static charge as it moves through the line—even a tiny spark from that can set it off. That’s why all our residue collection surfaces and cleaning tools are static-dissipating, and we add static dissipaters in areas where residue dust is common. Third, ignoring hidden residue. We’re talking about under conveyor supports, inside pipe elbows, on valves that are only opened once a day. A lot of lines only clean the “visible” parts, but that’s where the worst stuff builds up. We do line audits with thermal imaging and dust detectors to find those hidden spots, because residue doesn’t just sit in plain sight.
Before I wrap this up, let’s talk about why this isn’t just a safety thing—it’s a business thing. When you have consistent residue control, you get less product waste (no unexplained batches getting rejected because of cross-contamination), less unplanned downtime, lower labor costs for cleanup, and most importantly, a safety record that doesn’t keep OSHA (or whatever regulatory body you follow) breathing down your neck. We’ve had clients come to us after a year of working with us, and they say their production uptime is up 20% just because of residue management. That’s not small change.
At the end of the day, handling residues on an explosives production line isn’t about being perfect—it’s about being intentional. It’s not something you do once and forget about, it’s a daily, weekly, ongoing process that needs to be baked into how you run your line, not an afterthought. We’ve spent years refining our solutions because we’ve seen what works and what doesn’t, and we know that every line, every product, every team is different—so we don’t do generic fixes.

If you’re dealing with residue-related headaches—whether it’s safety scares, downtime, product issues, or just not knowing where to start—reach out to our team to talk through your specific line and needs. We don’t just sell equipment; we work with you to build a residue plan that fits your operation, no matter if you have a small 2-run line or a large-scale production facility. Don’t let residues hold your line back anymore—let’s figure this out together.
Underground Loading Trolley References:
- Center for Chemical Process Safety (CCPS). (2020). Guidelines for Safe Handling of Explosive Residues in Manufacturing Operations. American Institute of Chemical Engineers.
- Occupational Safety and Health Administration (OSHA). (2019). Safety Standards for Explosives Manufacturing and Storage (29 CFR 1910.109). U.S. Department of Labor.
- European Council for Laboratories and Special Materials (ECLSM). (2021). Best Practices for Residue Management in Commercial Explosives Production. ECLSM Technical Report Series.
Shanxi Honghu Special Purpose Vehicle Manufacturing Co., Ltd.
As one of the most professional explosives production line manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk explosives production line in stock here and get pricelist from our factory. Also, custom service is available.
Address: No. 16 Nanhuan West Street, Changzhi Economic and Technological Development Zone, Shanxi Province
E-mail: sxczhh15035590669@163.com
WebSite: https://www.mixedexplosivestruck.com/
